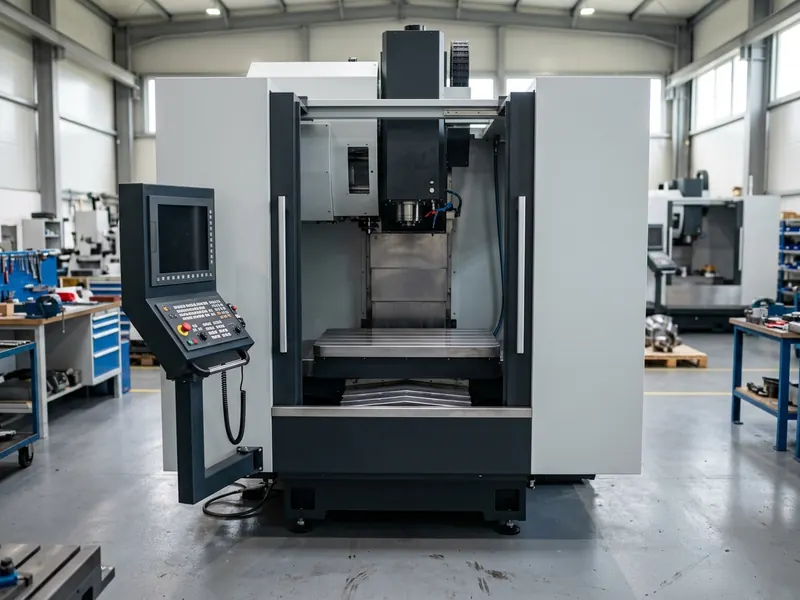
VMC650 · VMC850 · VMC855
VMC Vertical Machining Centers
C-frame vertical milling centers with BT40 spindles, 24-tool servo ATC, and preloaded roller linear guideways.
650–855 mm X-Travel · BT40 · 10,000 RPM · ±0.003 mm
View Series SpecificationsISO 230-2 Laser Calibrated · Direct Factory Supply
HT300 cast-iron beds, P4 spindle bearings, and ±0.003 mm positioning repeatability. Configured with FANUC or Siemens controls for continuous production.
±0.003 mm
Repeatability
ISO 230-2 laser interferometer verified
12,000 RPM
Max Spindle Speed
BT40 direct-drive & belt-drive options
9 Models
Product Lineup
VMC650–855 · TCK50–56 · CK6140–6160
24 Hours
Quotation Turnaround
Tooling layout, cycle study & FOB/CIF pricing
Machine Catalog
Select the machine series suited to your workpiece envelope, batch size, and material hardness.
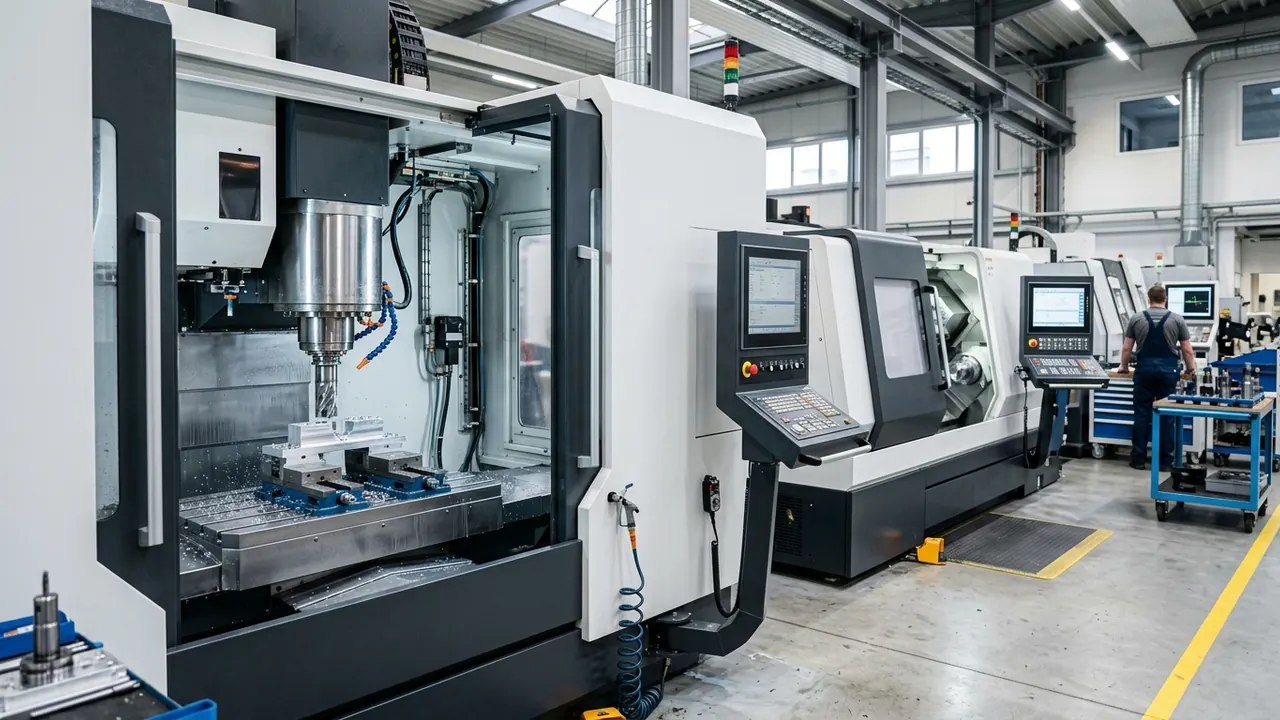
C-frame vertical milling centers with BT40 spindles, 24-tool servo ATC, and preloaded roller linear guideways.
650–855 mm X-Travel · BT40 · 10,000 RPM · ±0.003 mm
View Series Specifications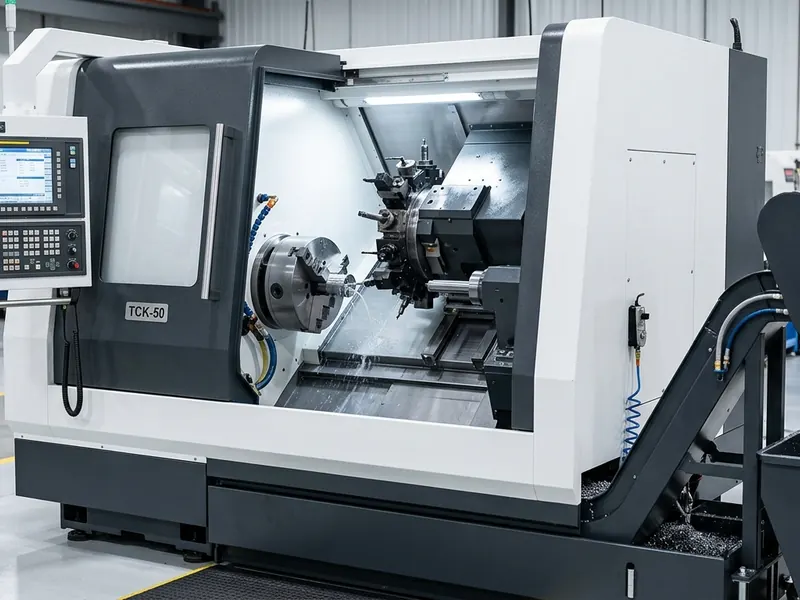
Monoblock 45° slant-bed turning centers with hydraulic chucks, 12-station servo turrets, and programmable tailstocks.
45° Slant Bed · 500–560 mm Swing · 4,000 RPM · Hydraulic Turret
View Series Specifications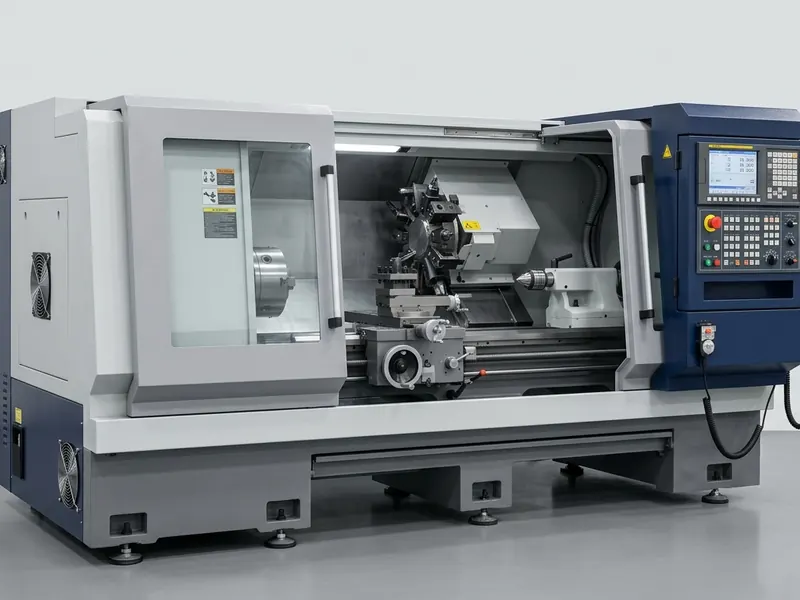
Induction-hardened (HRC 52+) wide box-way horizontal lathes built for heavy shaft turning, oilfield couplings, and rollers.
400–600 mm Swing · HRC 52+ Hardened Ways · Ø82–105 mm Bore
View Series SpecificationsSpecifications
Key capacity, spindle, and accuracy parameters across all 9 models.
Construction & Quality
Every machine is built around cast-iron mass, thermal stability, and documented geometric inspection.
Castings
Beds, columns, and saddles are cast from HT300 gray iron and furnace-annealed twice to remove internal casting stress before guideway grinding.
0.005 mm / 1000 mm guideway straightness
Spindle & Feed
Spindle cartridges are assembled in a temperature-controlled cleanroom using matched P4 bearings and pretensioned C3 ground ball screws.
≤ 0.002 mm spindle taper runout
Inspection
Each machine undergoes bidirectional pitch-error compensation per ISO 230-2, ballbar circularity testing, and a 48-hour continuous run test.
Serialized inspection report included
Sales & Application Engineering
Complete the 3 fields below and our engineering team will respond promptly.
Official B2B Inquiry Email
xiuc32860@gmail.comEvery inquiry is reviewed by a senior CNC application engineer to ensure correct chuck size, spindle torque, and transformer voltage for your facility.
Sales & Application Engineering
Complete the 3 fields below and our engineering team will respond promptly.